
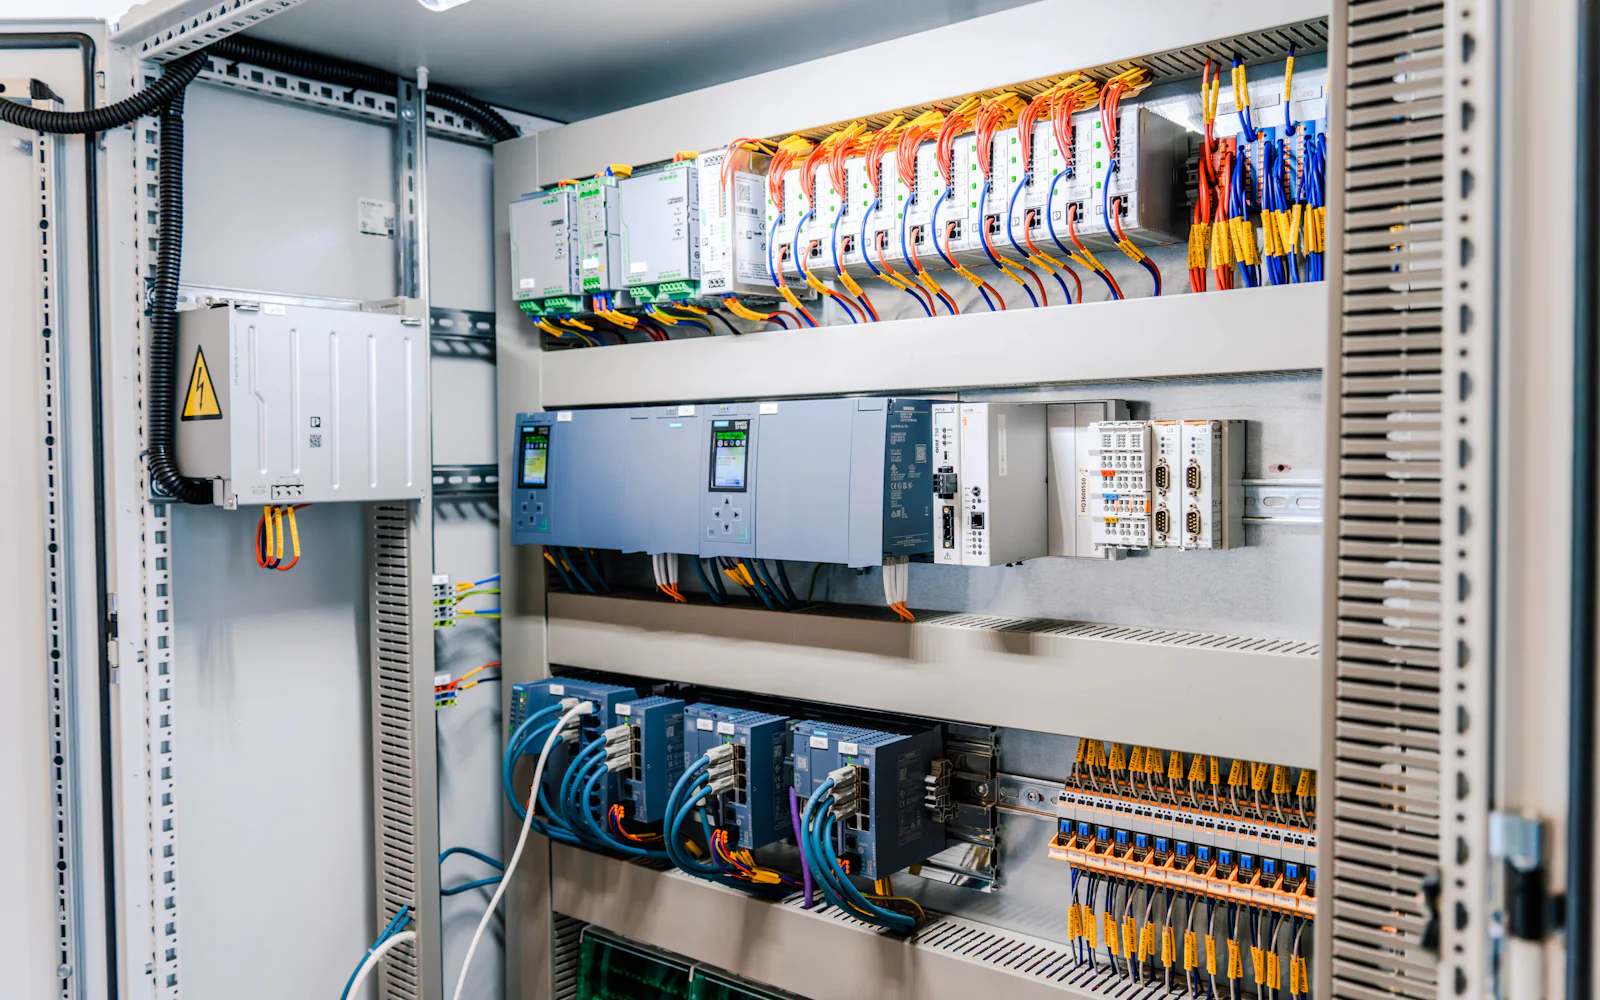
PLC programming services
Siemens and Allen-Bradley PLC programming for new machines, old relay panels and ageing S7-300 systems, written so your own engineers can read it after we leave.
What we program
A PLC is the part of the plant that makes decisions thousands of times a second: start this motor, open that valve, stop everything if the guard opens. Good PLC programming is the difference between a line that runs all season and one that trips every shift. We offer PLC programming services in Pakistan nationwide, and if you need a PLC programmer in Rahim Yar Khan, southern Punjab or upper Sindh, our team is close by. We write, fix and upgrade programs mainly on two platforms:
- Siemens PLC programming — S7-300, S7-400, S7-1200 and S7-1500, using TIA Portal and STEP 7 Classic.
- Allen-Bradley PLC programming — ControlLogix and CompactLogix with Studio 5000 / RSLogix 5000.
- Retrofit work on Delta, Schneider and Mitsubishi PLCs where they are already installed.
Typical PLC jobs
New machine or line
We start from your process description and the I/O list, then write the logic in clear, commented blocks: one standard block for every motor, valve and analog signal, with interlocks, alarms and manual/auto modes handled the same way everywhere.
Relay panel to PLC retrofit
Old relay and timer panels are hard to fault-find and impossible to change. We trace the existing wiring, turn it into PLC logic, and keep the same push-buttons and lamps where operators are used to them, so the change is easy on the shop floor.
S7-300 to S7-1500 migration
Siemens has moved the S7-300 family into its phase-out cycle, and spare CPUs are getting expensive. We migrate STEP 7 projects to TIA Portal, re-test every interlock and plan the switch-over for a shutdown. Read our S7-300 migration guide for the full checklist.
PLC troubleshooting and fault finding
When a machine stops and nobody knows why, we go online with the PLC, follow the logic from the stopped output back to the missing condition, and fix the root cause instead of forcing bits.
What you receive
- The final PLC program, fully commented, plus a backup copy on your plant PC.
- An I/O list and alarm list in Excel.
- Short training for your electricians on how to read the program and find faults.
- Matching SCADA and HMI screens if the job needs them.
FAQ
Straight answers to what plant owners and engineers ask us most.
How long does an S7-300 to S7-1500 migration take?
For a single machine with a few hundred I/O, design and testing usually take two to four weeks, and the cut-over itself is planned for a shutdown so production loses as little time as possible.
Can you work on a PLC when we don't have the original program?
Usually yes. We upload the program from the running PLC, add comments and symbols as we work through it, and give you a documented copy at the end.
Do you write programs to a standard?
Yes. We use IEC 61131-3 languages (ladder, function block, structured text), consistent tag naming, and reusable blocks for motors, valves and analog inputs so any engineer can maintain the code later.
Machine down or planning an upgrade?
Send us the PLC model and the problem. We reply within one working day.